Tooling amortisation decides the long-term viability of filigree patterns. Lower-cost molds result in thinner wall thickness but increase the failure rate at the solder joints over a 24-month retail cycle.
Replacement rate, not unit price, dictates the actual margin on high-volume contracts. Thin-gauge metal filigree often buckles under stress in high-humidity environments where the metal expands. Selecting a die-cast zinc alloy over stamped iron ensures the intricate pattern maintains its geometric alignment during transit.
Assumptions Buyers Should Stop Making
| Parameter | Technical Specification |
|---|---|
| Substrate Material | Cold-rolled iron or Die-cast zinc alloy |
| Glass Thickness | 4mm to 6mm float silvered glass |
| Filigree Attachment | Electro-welded or precision-bonded |
| Finish Process | Gold-ion electroplating or metallic-powder coating |
The total cost of ownership shifts once returns are counted. Many buyers overlook the weight of the mirror assembly, which leads to mounting failures if the frame hardware is not rated accordingly. A reinforced rear-cross-bar prevents the glass from bowing, which maintains the silvering integrity over time.
The filigree design often serves as a weak point for oxidation. If the gold finish lacks sufficient thickness, moisture penetrates the iron substrate and triggers galvanic corrosion. We specify a 5-micron electroplating layer to mitigate this risk in coastal retail environments.
Customisation Options and Their Limits
Electroplated Finish
Provides the highest metallic luster for fine filigree details. It is susceptible to abrasions if the cleaning agents used by the end-consumer are acidic.
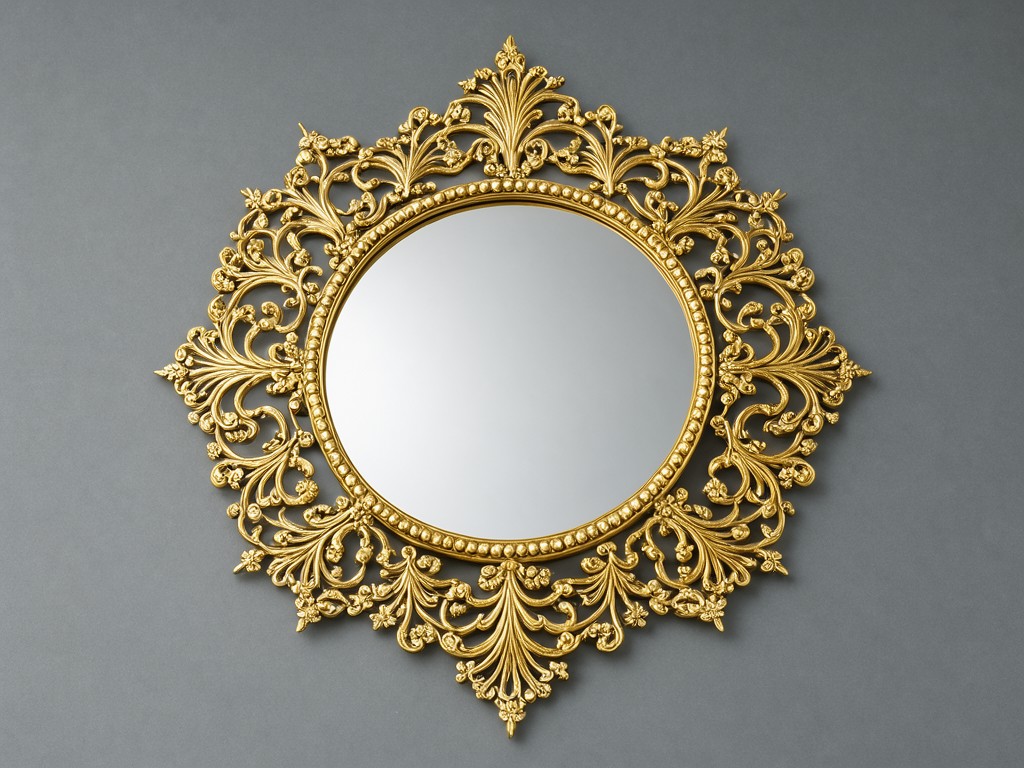
Powder Coated Gold
Offers superior impact resistance and durability. However, the coating thickness may obscure the sharp edges of intricate metalwork compared to electroplating.
Complexity in the filigree pattern directly impacts the assembly speed. High-density patterns require manual soldering points, which increases the probability of thermal stress fractures in the frame. We limit filigree density to machine-cut geometries to ensure structural consistency across large production batches.
Inspection Items and Test Methods
Mirror stability is verified through impact testing of the glass bond. We utilize a vibration table to simulate transit stresses and ensure the glass does not rattle against the filigree frame. If the adhesive bond shows separation at even 1mm, the batch is flagged for reinforcement failure.
Quality Assurance Protocol
- Salt Spray Test: 48-hour exposure to validate the gold-finish corrosion resistance.
- Adhesion Test: Cross-cut tape test on the mirror backing to prevent delamination.
- Dimensional Check: Verification of frame squareness within ±1.5mm across the diagonal.
- Weight Variance: Ensuring each unit matches the specification for shipping-cost accuracy.
Keeping Repeat Orders Supplied
Consistency in the finish tone is the primary driver for repeat wholesale orders. Variations in the gold hue between production runs can cause visual mismatches in multi-unit retail displays. We utilize master-batch color matching to ensure the optical properties remain constant across different manufacturing cycles.
Reliable logistics require de-risking the shipping process. By implementing custom foam-molded inserts, we reduce the claim rate of shattered glass to under 1%. This stability allows procurement managers to review the branding standards without fearing inventory loss.
Packing, Marking and Freight Configuration
Standard cardboard boxes are insufficient for filigree mirrors due to point pressure risks. We utilize reinforced plywood crates with internal corrugated-board dividers to prevent the metal frames from scratching one another. Moisture-barrier foil is included to prevent desiccation issues during long-haul sea freight.
Each pallet is marked with a barcode containing the batch number, material grade, and weight distribution. This traceability allows for rapid isolation if a material defect is identified in the field. Proper palletization ensures that the center-of-gravity remains low, preventing tipping during container loading.